A 3-axis vertical machine, 600 x 400 x 400 mm travel, designed in Whet: the audit, the solver runs and what is left open.
CNC machining centre
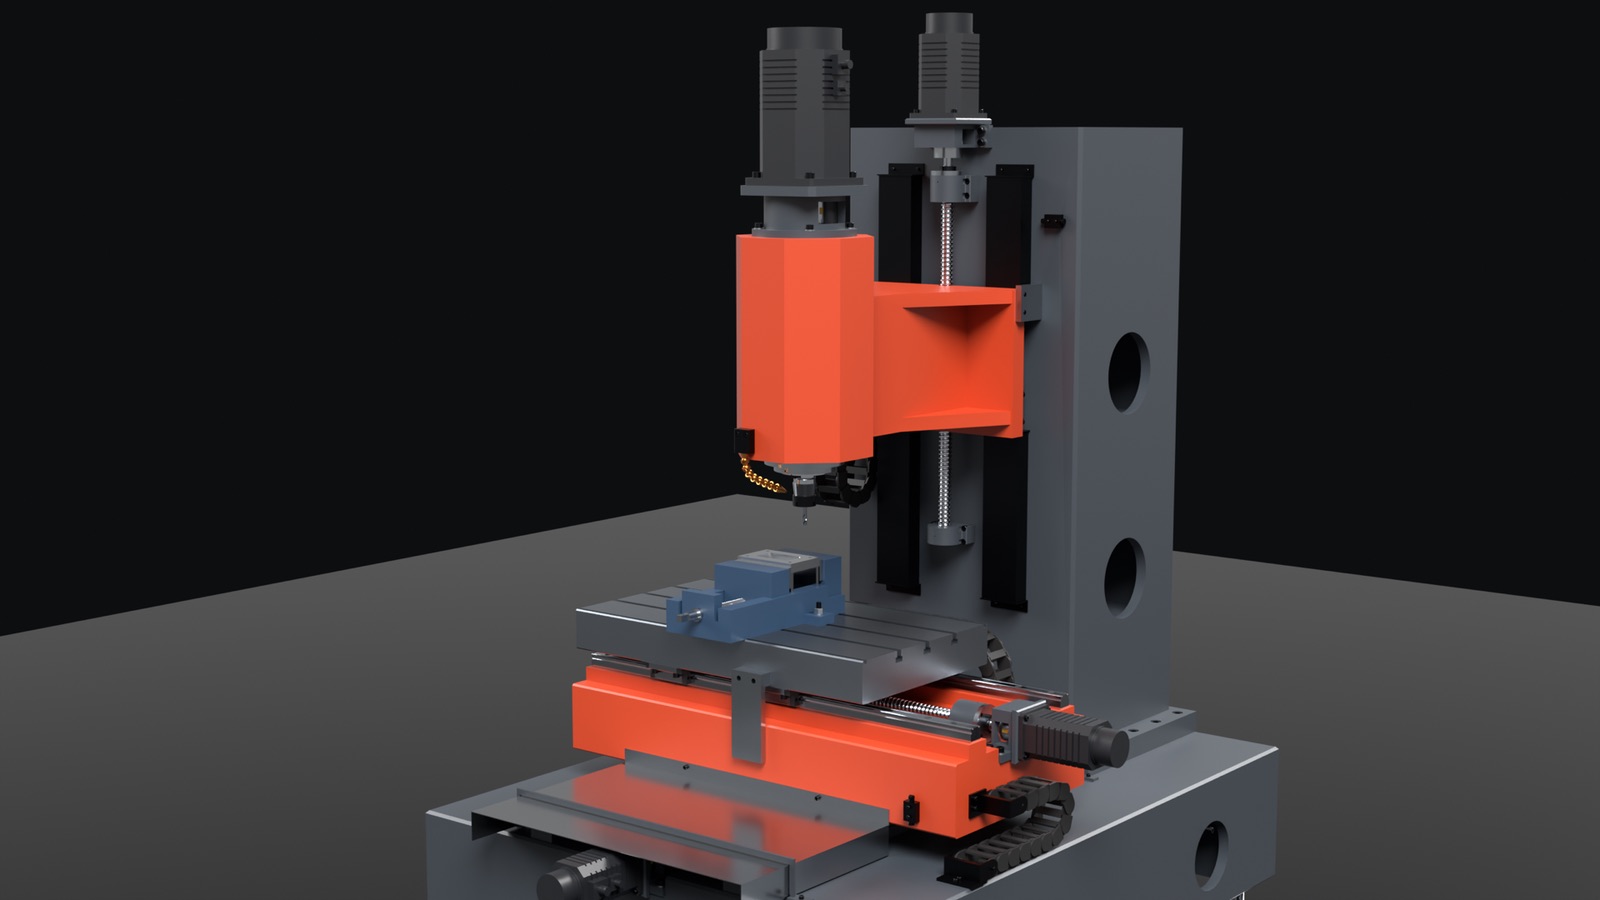
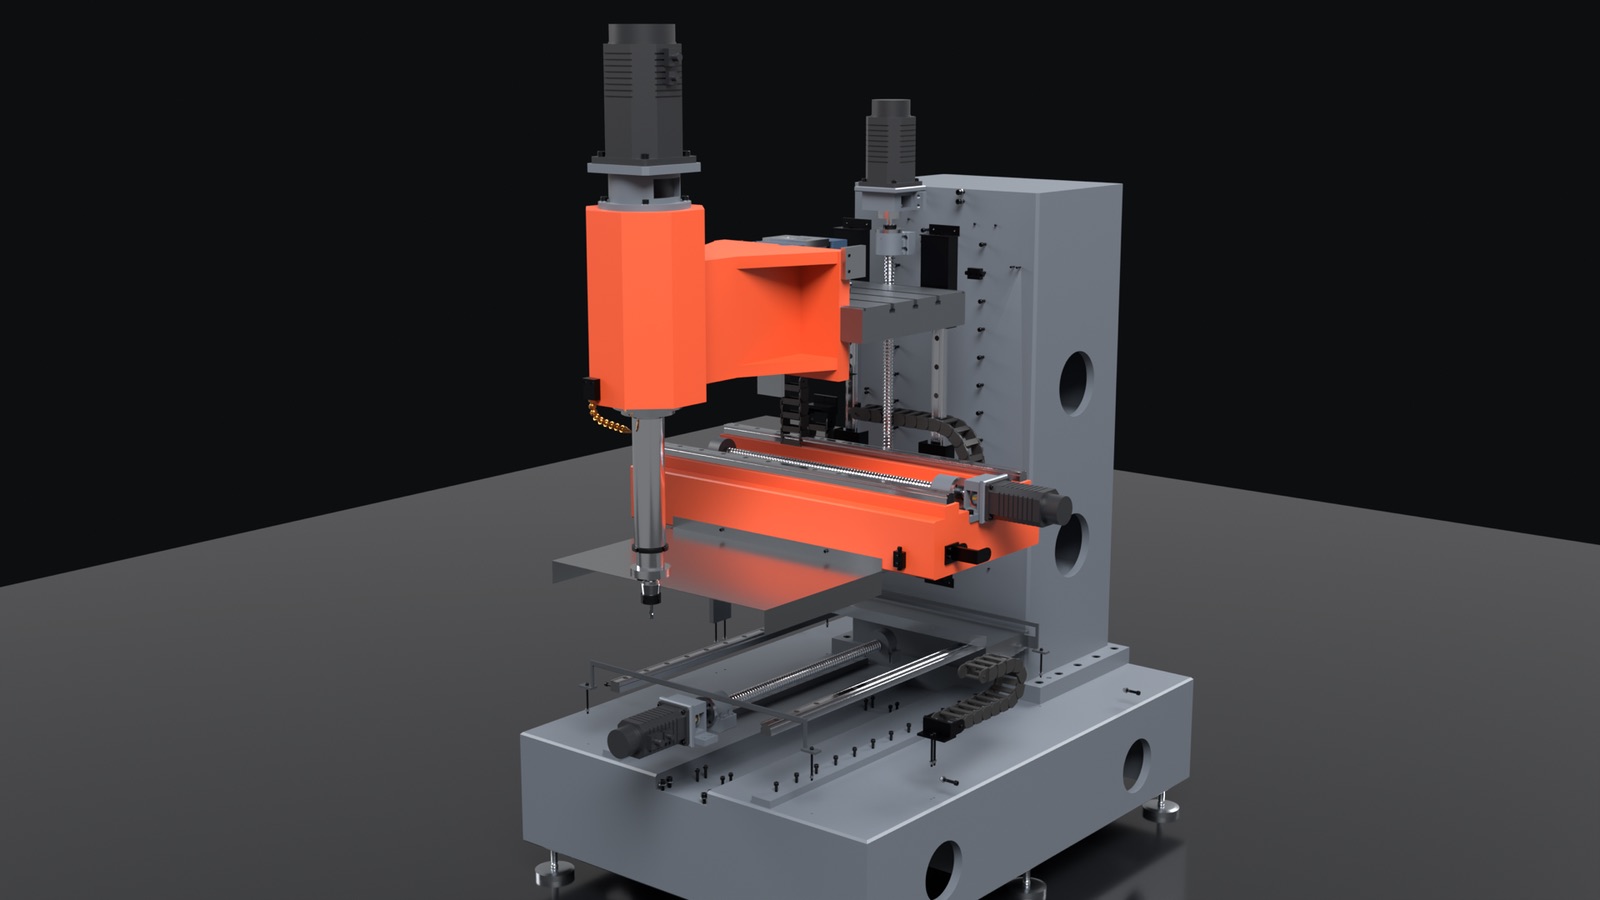
A 3-axis vertical machine, 600 x 400 x 400 mm travel: 1016 parts, 433 threaded fasteners.
Designed in Whet: 1016 parts from 167 kernel-built specs, 433 threaded fasteners each in its own modelled thread. Audit: 0 unpaired, 0 overlaps, 0 floating. cnc-hero, 2026-10-06
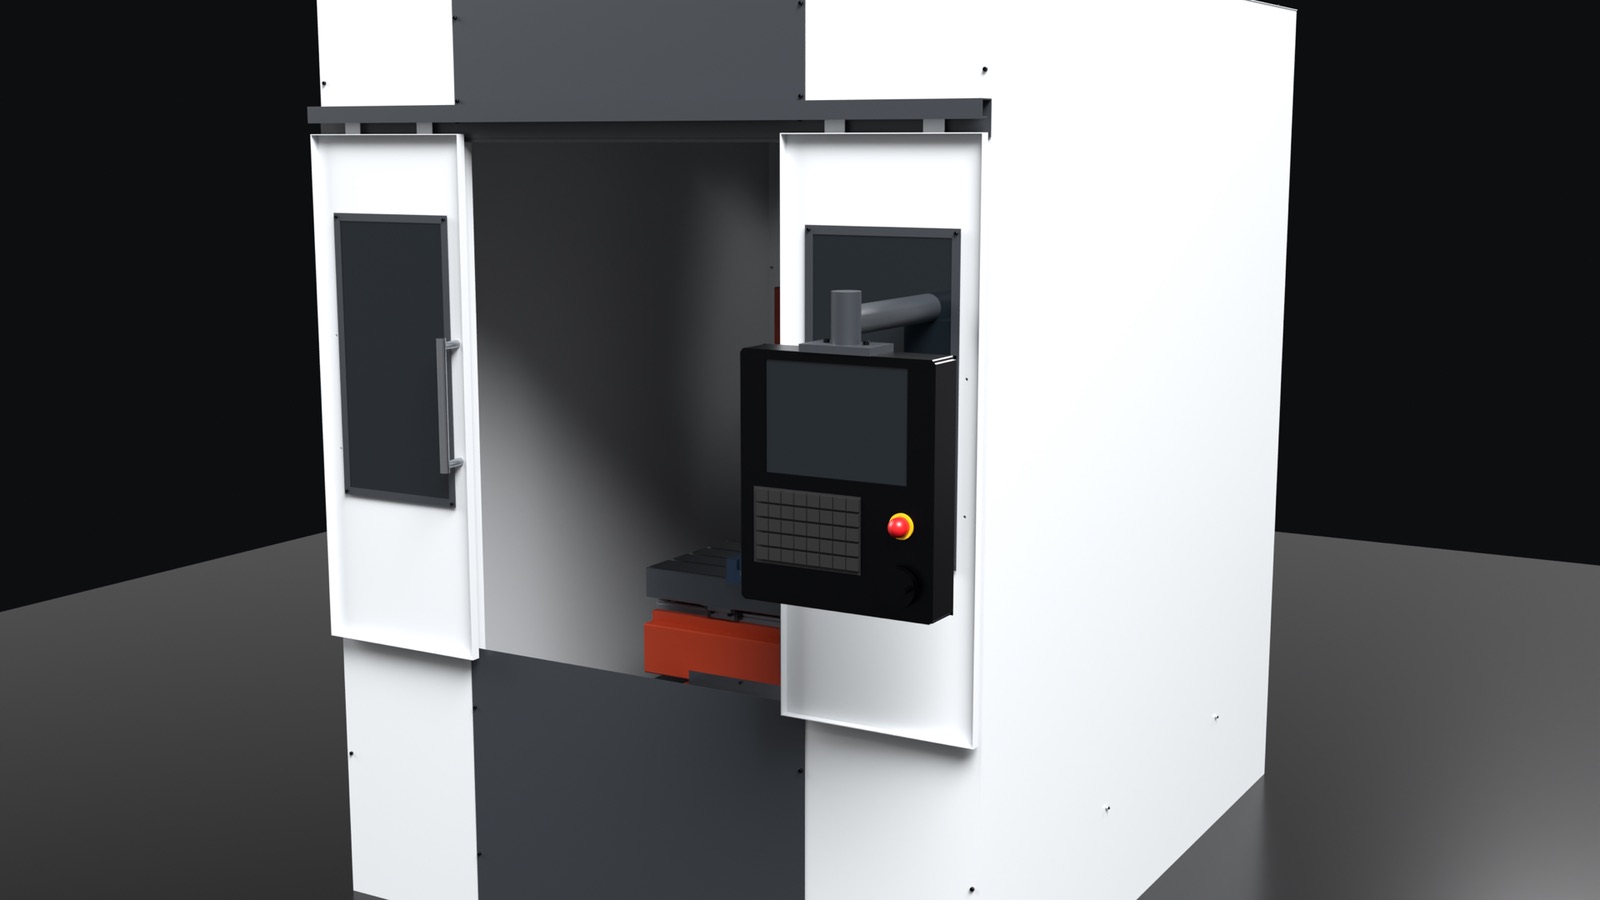
The machine in its sheet-steel enclosure with both doors slid open and the pendant on its swing arm. cnc-enclosure-open, 2026-10-06
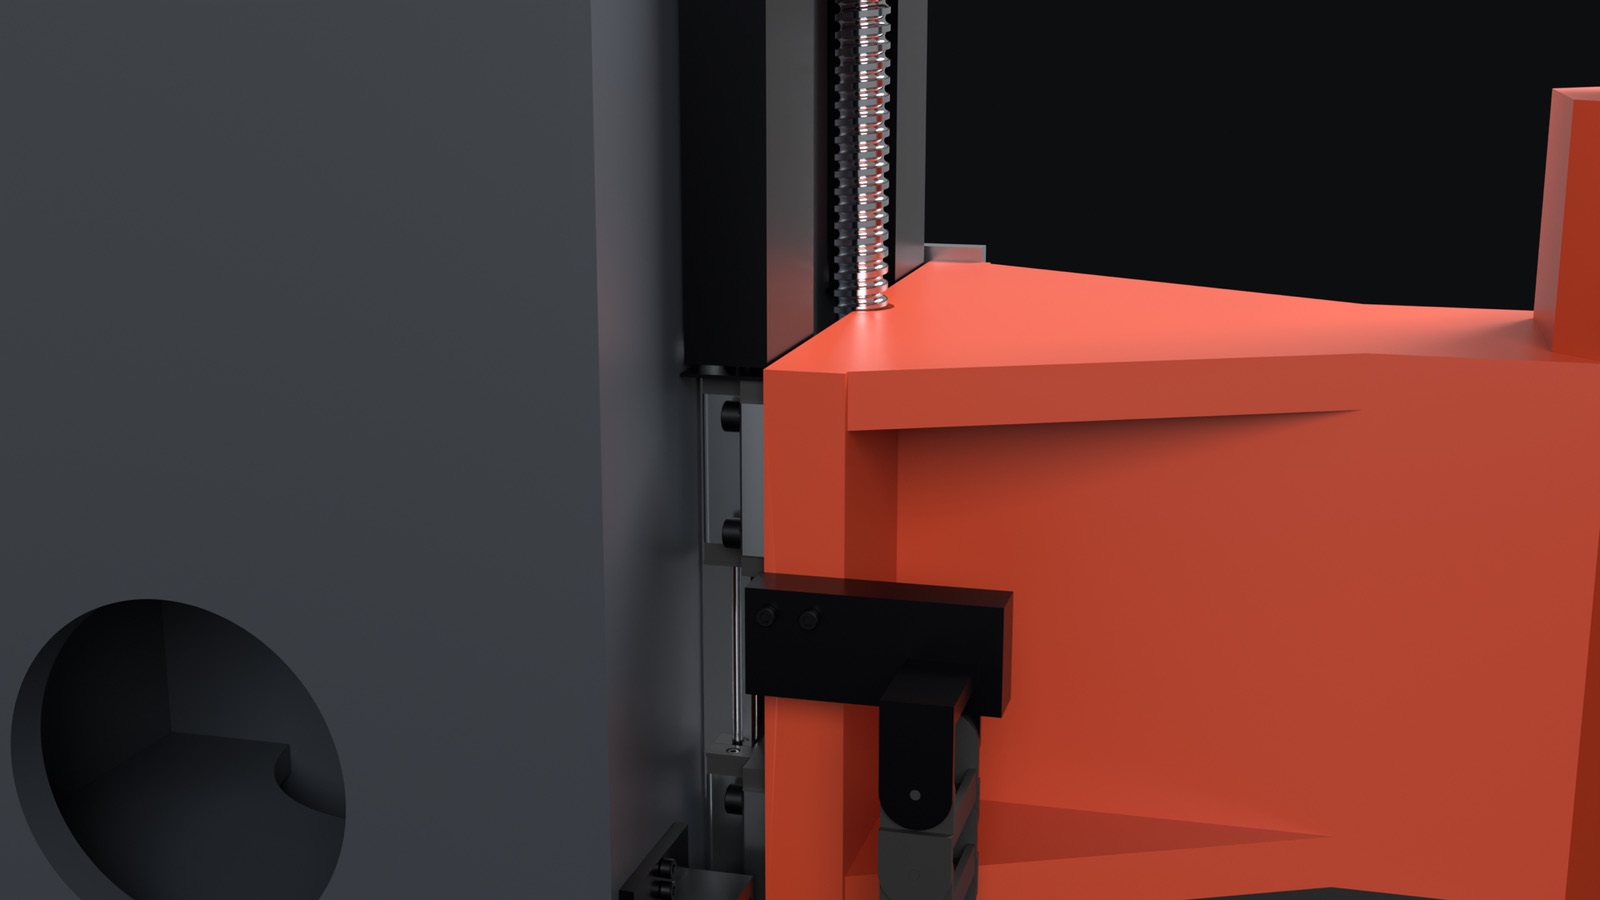
The Z axis: size-35 rails, a 32 x 10 ball screw between a fixed 7205-pair support and a floating 6204 support, rail bellows and the cable carrier. cnc-z-axis, 2026-10-06
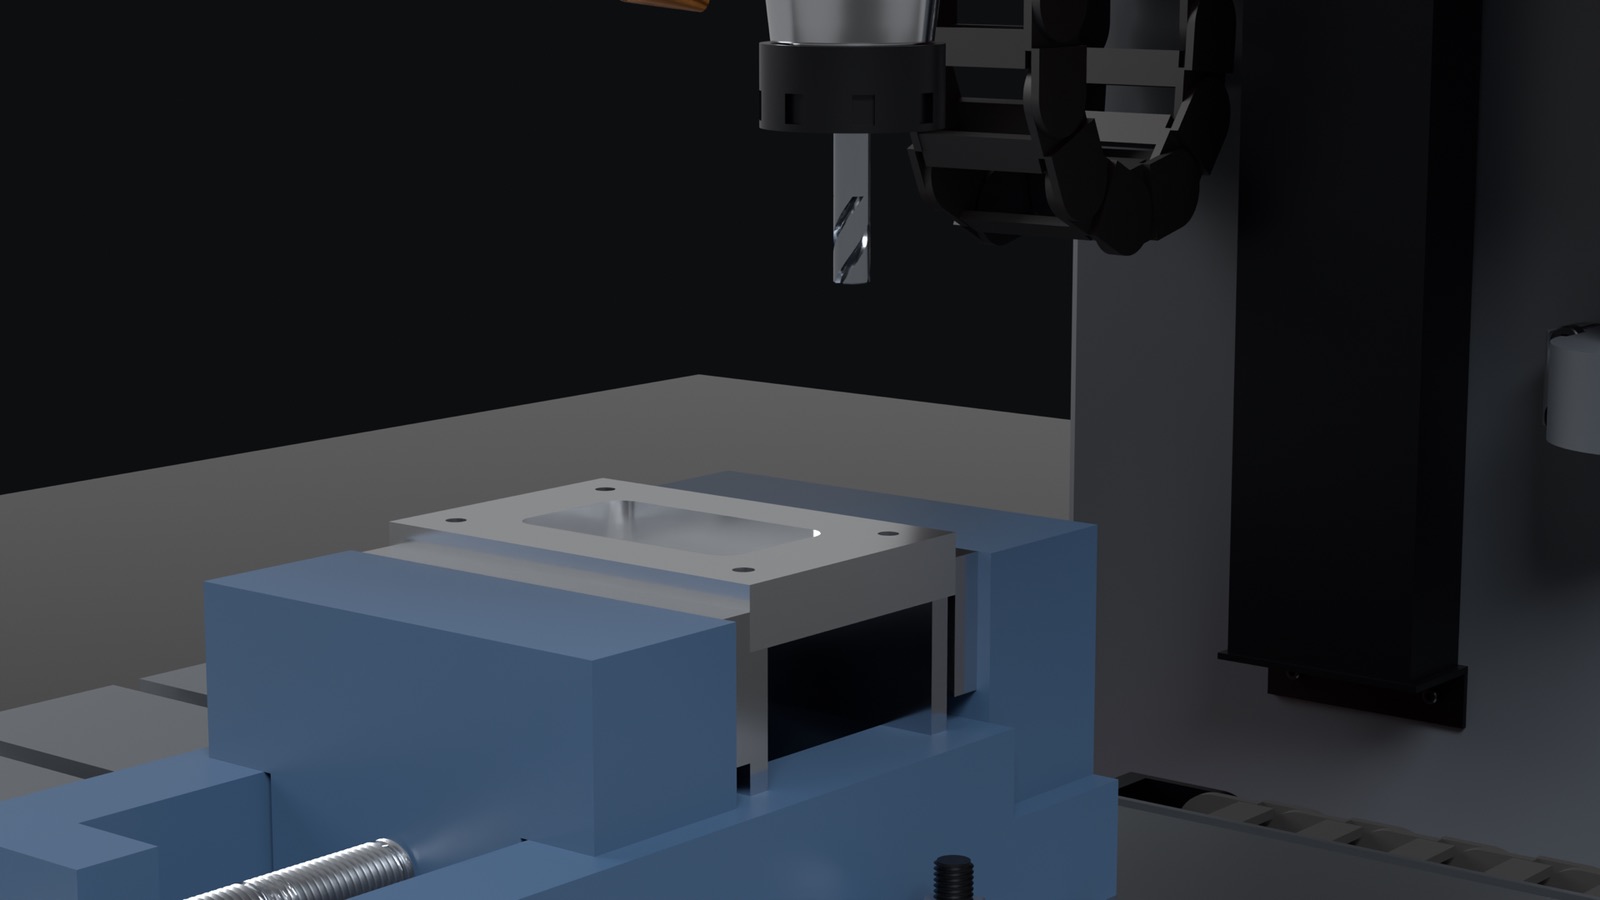
The BT30 / ER32 holder and a 10 mm three-flute end mill over the 150 x 100 x 20 aluminium plate in a 150 mm vise. cnc-spindle-part, 2026-10-06
The axis groups moved apart along their own slides: frame, Y ways, saddle, table, Z ways, head and spindle. cnc-exploded, 2026-10-06
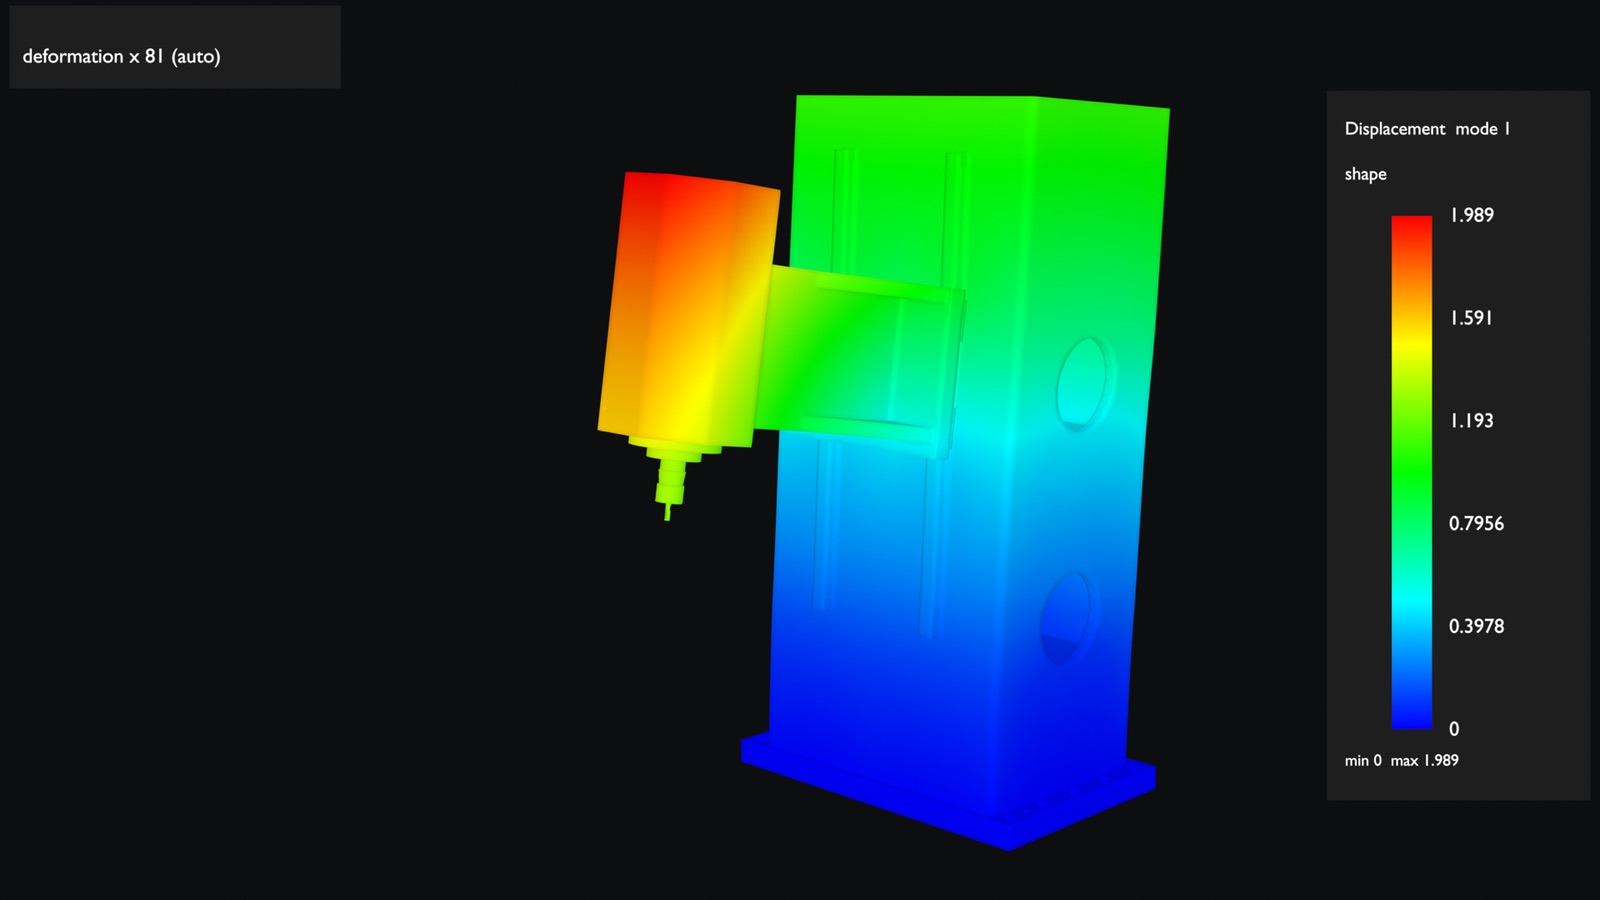
Column, Z ways, head and spindle held at the column foot: first natural frequencies 84.2, 95.1, 145.0 and 156.9 Hz (CalculiX, 129,980 nodes, 1312 kg). cnc-modal-mode1, 2026-10-06
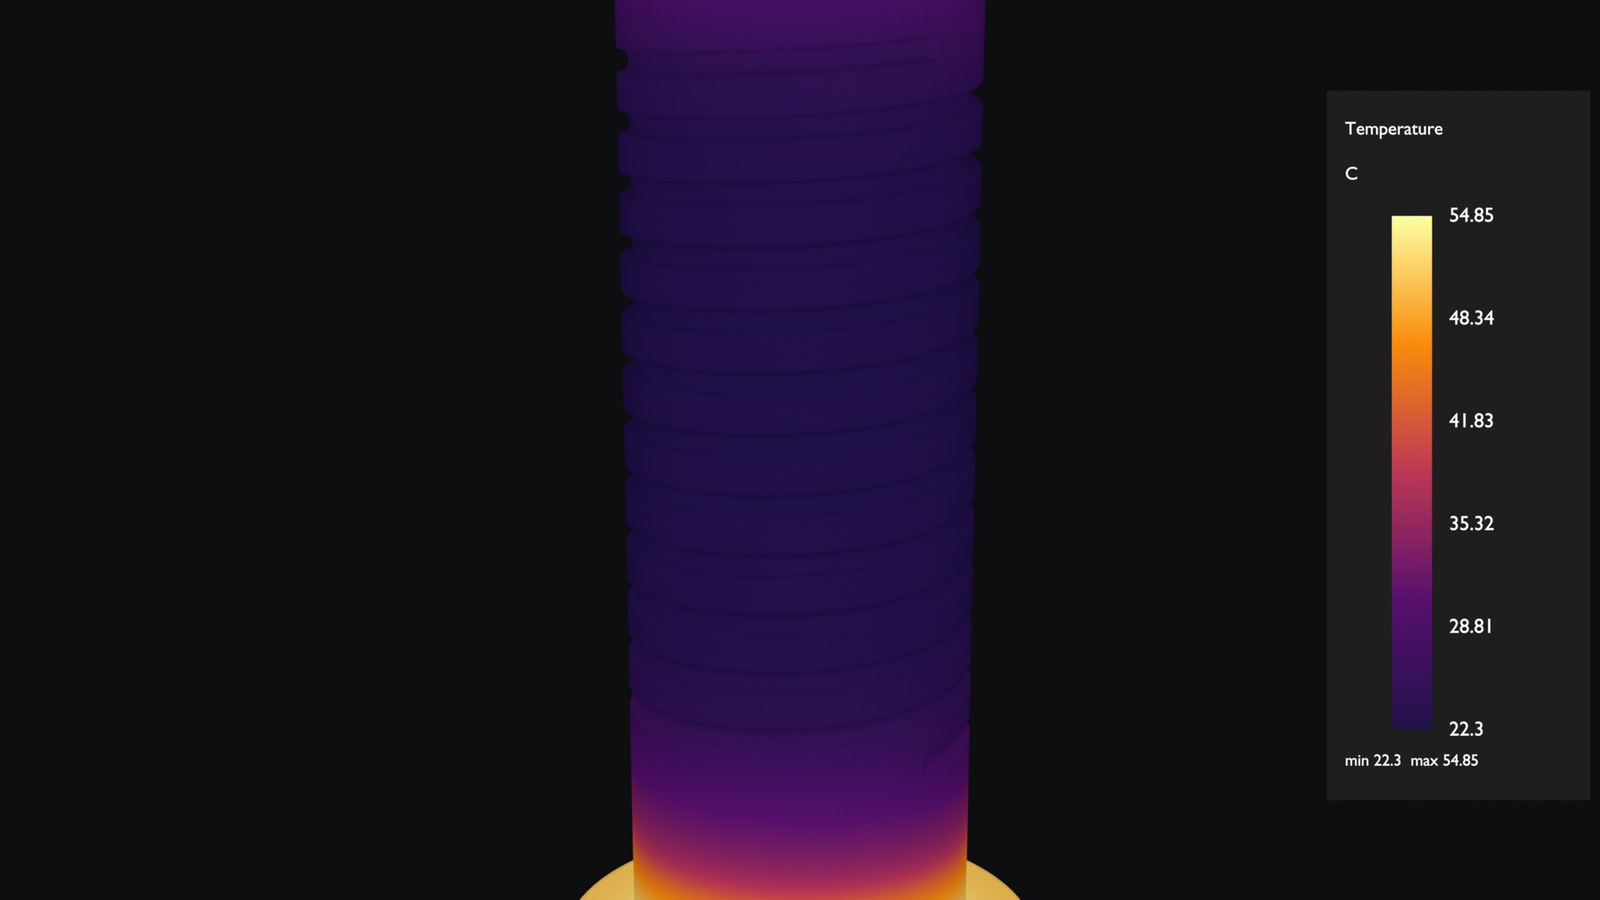
Spindle cartridge with 220 W into the front bearing seat and 80 W into the rear, a chilled-oil jacket at 22 C: 54.9 C peak at the front bearings. cnc-spindle-heat, 2026-10-06
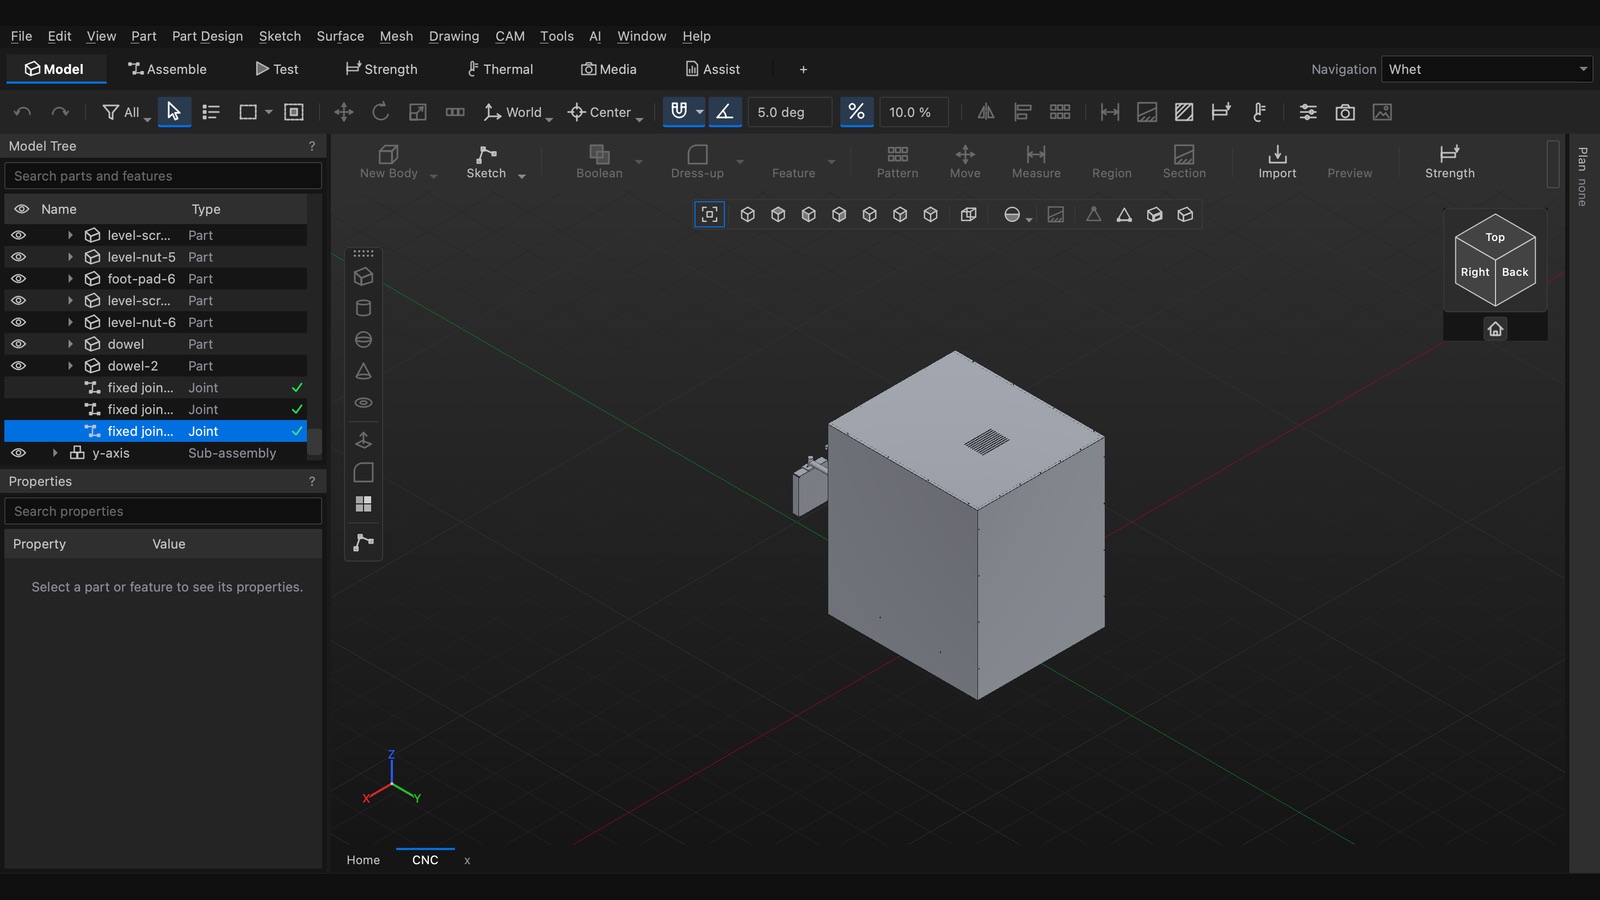
The machine opened in the Whet window with its model tree open at the frame: level screws, nuts, foot pads, dowels and three fixed joints, then the y-axis sub-assembly. cnc-window-model-tree, 2026-10-08
What was checked
1016 parts placed, from 167 part specs built by the kernel.
433 threaded fasteners checked on the real parts with their threads. Unpaired: 0. Screws with material on their own axis: 0.
Engaged: 222 in a tapped hole in a casting, 108 in a tapped hole in a part, 103 in a nut.
Interference: 515,620 part pairs, 2,502 with boxes that meet. Overlapping past 1e-6 mm3: 0. Pairs the kernel could not evaluate: 0.
Contact: 986 parts touching, 30 within a running clearance (the chain links), floating: 0.
459 tapped holes cut with an internal ISO 262 thread.
cnc-audit, 2026-10-01
What was computed
Natural frequencies of column, Z ways, head and spindle held at the column foot: 84.2, 95.1, 145.0 and 156.9 Hz (CalculiX, 129,980 nodes, 1312 kg).
Stiffness for 1 kN at the tool tip, column side only: X 7.3 N/um, Y 6.9 N/um, Z 78 N/um.
Spindle cartridge with 220 W into the front bearing seat and 80 W into the rear, a 2000 W/m2K jacket at 22 C: 54.9 C peak at the front bearings, heat balance off by 0.02 W.
CAM: face, pocket and profile operations posted as G-code, 394 s of program. The MuJoCo run that followed it: worst lag 2.4 mm on 15 m/min rapids, 0.25 to 0.65 mm RMS.
cnc-modal-mode1, 2026-10-06
Reference
A 3-axis vertical machining centre with a BT30 spindle and ER32 collets, size-35 rails, a 32 x 10 ball screw, and standard parts by ISO and DIN number. Nothing here names a real machine; this is a design.
cnc-audit, 2026-10-01
Not done yet
The audit is the machine at one position, X 0, Y 0, Z 0. Nothing is swept through the travel.
The MuJoCo run moves the three axis groups as blocks, so it says nothing about clearance between parts.
Thread engagement is shown by a point test, not by a boolean.
No tolerance, fit class or surface finish is modelled.
The spindle loads are typed, not measured.
The film of the machine and the stiffness still are not finished.
 Whet